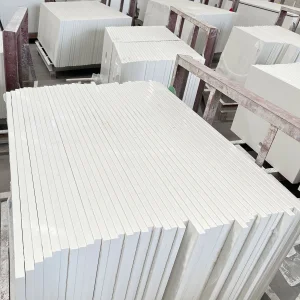
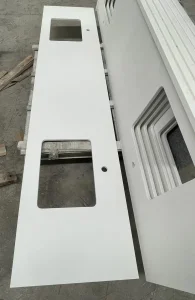
Explore our top-tier engineered quartz surfaces specifically curated for premium residential and commercial applications in the Ebeye market.
Rooted in Nanan, China’s preeminent stone manufacturing nexus, delivering uncompromised architectural integrity worldwide.
Nanan Zenlith Co., Ltd. is a professional manufacturer and global supplier specializing in artificial marble, quartz stone, and engineered & natural stone solutions for residential, commercial, and architectural applications. Based in Nanan—one of China’s most established stone industry hubs—the company integrates advanced production technology with strict quality control to deliver consistent, high-performance surfaces.
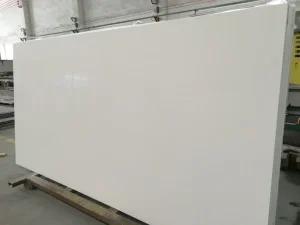
Operating state-of-the-art facilities equipped with Breton-inspired vacuum-vibration pressing lines, Zenlith ensures structural homogeneity and extreme impact resistance across all pure white quartz product lines destined for international markets like Ebeye.
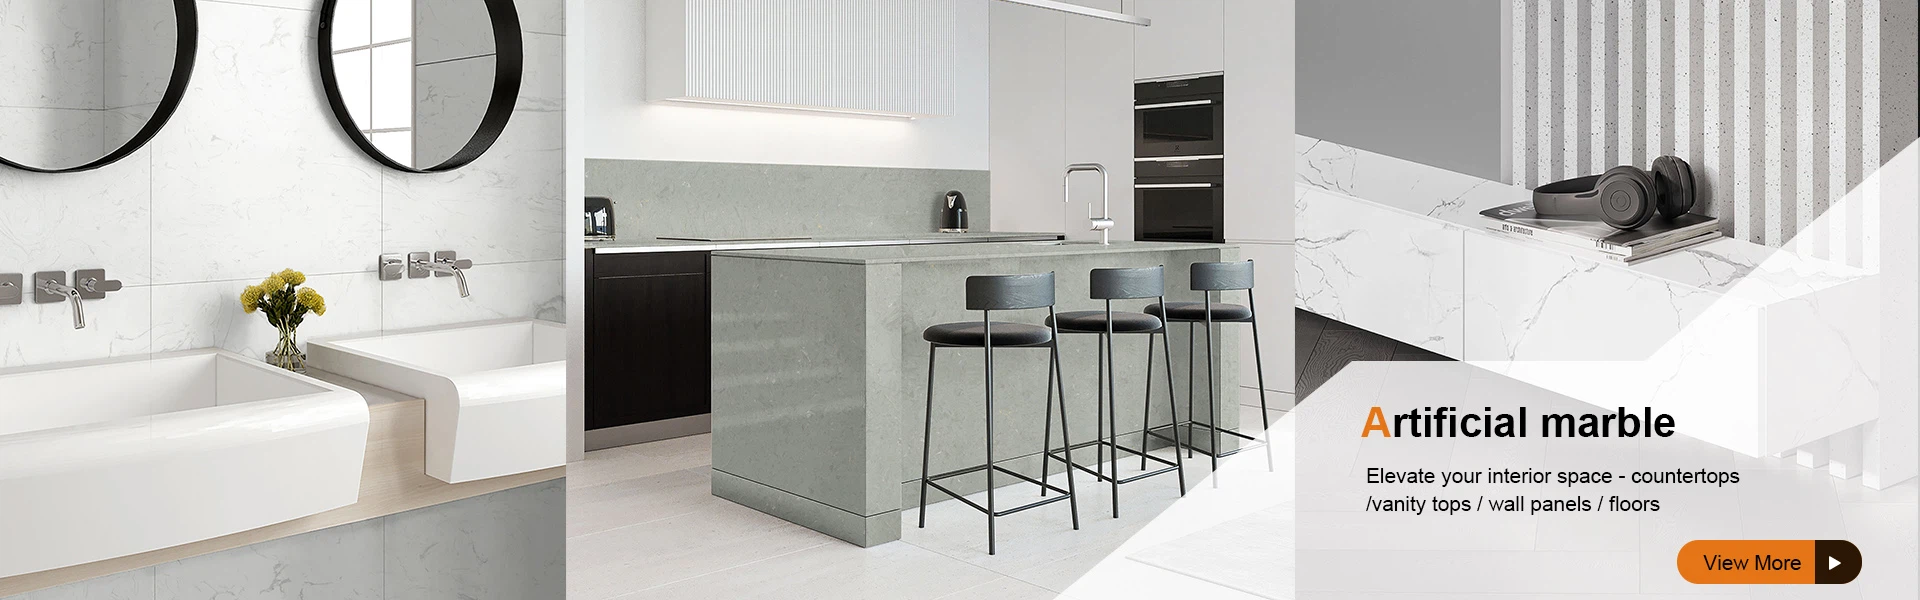
Zenlith’s product portfolio includes artificial marble slabs, engineered quartz surfaces, and a wide selection of natural stones such as granite and marble. Designed to meet modern design and construction demands, its materials are widely used for kitchen countertops, bathroom vanities, wall cladding, flooring systems, and custom interior projects. The company focuses on durability, stain resistance, and aesthetic versatility, offering a variety of colors, textures, and finishes tailored to global market trends.
With a commitment to innovation and sustainability, Zenlith continuously upgrades its manufacturing processes to ensure environmentally responsible production and long-term product reliability. Its experienced team provides OEM/ODM services, supporting clients from material selection and customization to packaging and export logistics.
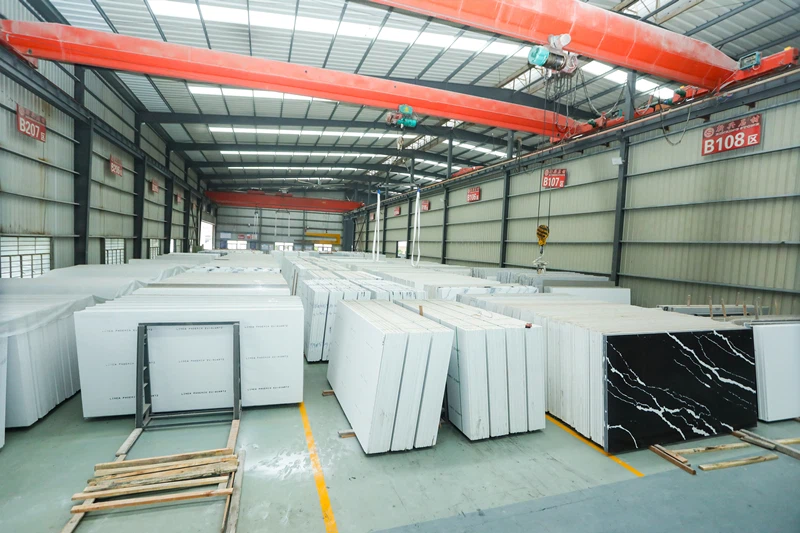
Serving customers across North America, Europe, the Middle East, Southeast Asia, and island economies including the Ebeye market, Nanan Zenlith Co., Ltd. has built a strong reputation for quality, competitive pricing, and dependable delivery—making it a trusted partner for stone solutions worldwide.
Understanding the unique architectural requirements, marine-climate resilience, and urban development trends shaping the Ebeye market.
Ebeye Island, known for its dense urban environment and strategic significance within the Marshall Islands, presents distinct infrastructural and interior design demands. In environments characterized by high humidity, coastal salinity, and tropical exposure, traditional building materials often degrade rapidly. Pure white quartz engineered stone offers an exceptional alternative, providing a non-porous, highly dense barrier against moisture ingress, mold proliferation, and salt corrosion.
Recent trends in residential upgrading and commercial hospitality developments in the region emphasize minimalist aesthetics, bright reflective surfaces that maximize spatial perception in compact layouts, and extreme hygiene. Zenlith's pure white engineered quartz slabs deliver zero-absorption performance (water absorption rate < 0.02%), making them impervious to tropical humidity and aggressive cleaning agents.
Rigorous quality assurance, advanced manufacturing formulations, and seamless export logistics tailored for overseas destinations.
As a premier factory and global supplier, Zenlith implements a strict 5-stage quality assurance protocol—ranging from raw mineral selection (93% high-purity natural quartz crystals) to polymer resin blending, vacuum compression, high-temperature curing, and precision diamond-edge calibration and polishing. For clients supplying projects in Ebeye, our logistics framework ensures seaworthy fumigated wooden crate packaging, reinforced edge protection, and comprehensive tracking from our Nanan warehouse to port delivery.
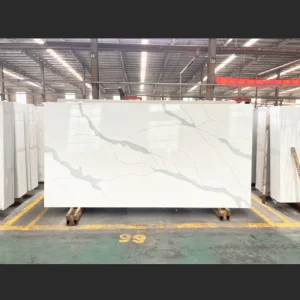
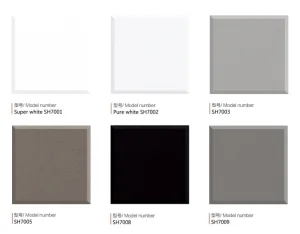
Browse our extensive range of engineered white quartz slabs, tiles, countertops, and vanity tops engineered for exceptional durability and timeless elegance.
Expert answers regarding our pure white quartz manufacturing, customization capabilities, and international shipping to Ebeye.
 Zenlith Stone