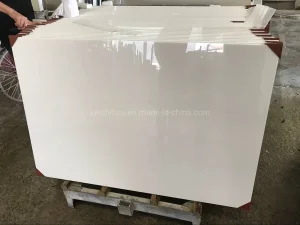
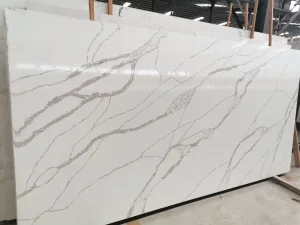
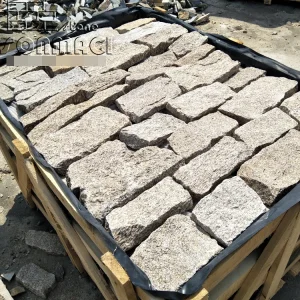
International architects, landscape contractors, and multi-national distributors demand uncompromising consistency in sizing, color saturation, and structural resilience. Whether sourcing raw pebble stones for urban riverbeds or engineered composite slabs for landmark hospitality projects, buyers look for suppliers who can guarantee bulk scalability without batch-to-batch variance.
Rooted in premier industrial clusters like Nanan, Chinese manufacturing ecosystems integrate advanced automated sorting machinery, massive quarry access, and highly streamlined logistics networks. This proximity to raw material sources allows suppliers to offer superior cost-efficiency, rapid mold customization, and flexible OEM/ODM manufacturing terms.
By establishing rigorous international distribution channels extending across North America, Europe, the Middle East, and Southeast Asia, top manufacturers maintain strict fulfillment standards. This ensures that custom orders arrive on schedule, packed securely to withstand rigorous maritime shipping and cross-continental freight.
Navigating international construction mandates requires absolute transparency in material composition. Leading manufacturers ensure all product batches comply with major international benchmarks, including CE marking, ASTM standards, and ISO9001 quality management systems. Rigorous laboratory testing for slip resistance, freeze-thaw durability, and chemical inertness guarantees that every stone performs seamlessly in high-traffic commercial environments and sensitive public spaces.
Pebble stones and advanced engineered solid surfaces find versatile roles across various architectural domains. From minimalist zen gardens and public pedestrian pathways in European municipalities to luxury resort pool decks in the Middle East and modern kitchen islands in North American residential homes, these materials provide both functional longevity and striking aesthetic contrast. Tailored finish options (polished, tumbled, or fluted) adapt effortlessly to regional architectural vernaculars.
The stone manufacturing sector is rapidly evolving toward circular economy models and digital fabrication. Forward-thinking suppliers are actively investing in water recycling systems, low-emission resin formulations, and dust extraction technologies to minimize environmental footprints. Furthermore, integration with 3D design software and digital prototyping allows architects to pre-visualize custom pebble layouts and engineered slabs with pinpoint precision, reducing job-site waste and shortening construction timelines worldwide.
Nanan Zenlith Co., Ltd. is a professional manufacturer and global supplier specializing in artificial marble, quartz stone, and engineered & natural stone solutions for residential, commercial, and architectural applications. Based in Nanan—one of China’s most established stone industry hubs—the company integrates advanced production technology with strict quality control to deliver consistent, high-performance surfaces.
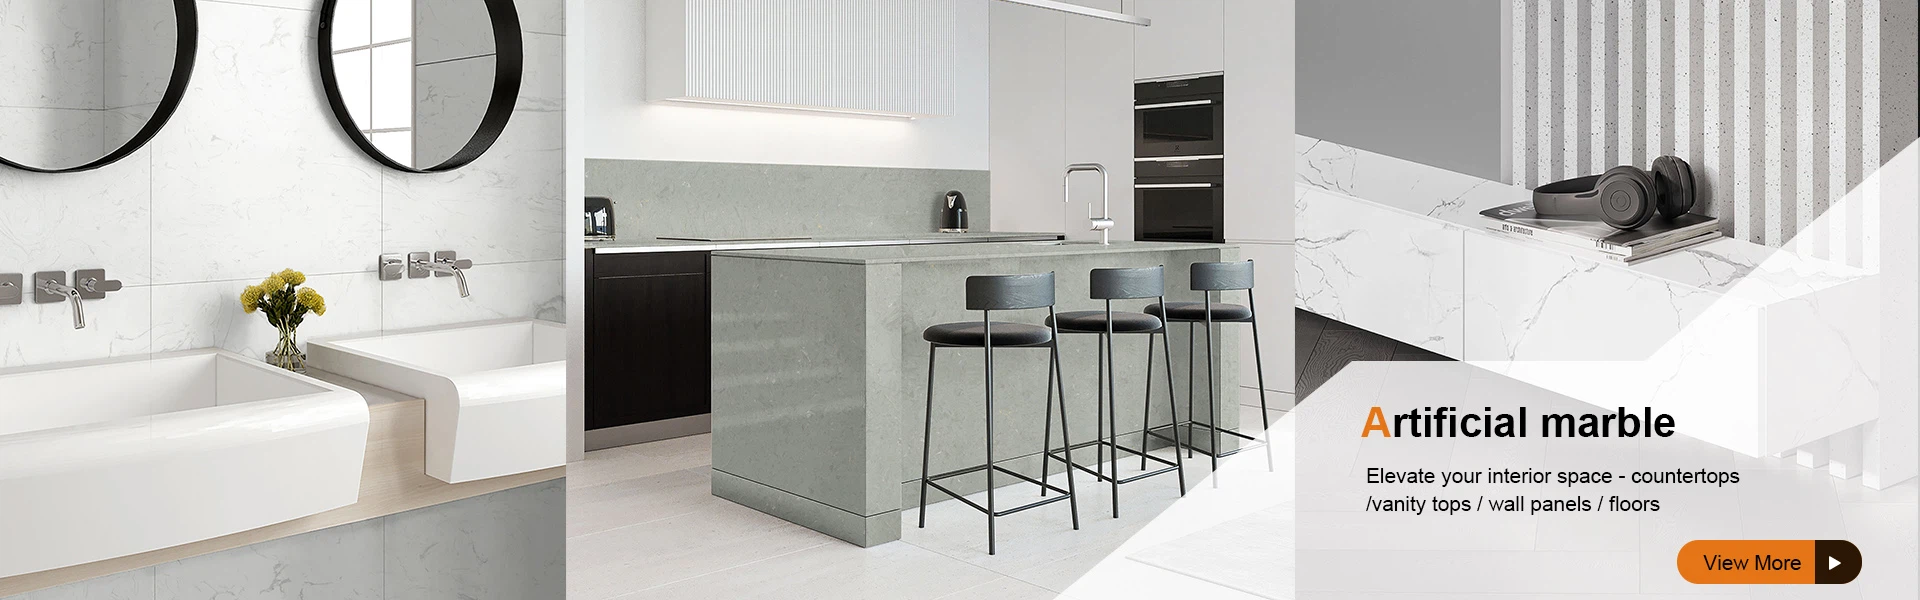
Zenlith’s product portfolio includes artificial marble slabs, engineered quartz surfaces, and a wide selection of natural stones such as granite and marble. Designed to meet modern design and construction demands, its materials are widely used for kitchen countertops, bathroom vanities, wall cladding, flooring systems, and custom interior projects. The company focuses on durability, stain resistance, and aesthetic versatility, offering a variety of colors, textures, and finishes tailored to global market trends.
With a commitment to innovation and sustainability, Zenlith continuously upgrades its manufacturing processes to ensure environmentally responsible production and long-term product reliability. Its experienced team provides OEM/ODM services, supporting clients from material selection and customization to packaging and export logistics.
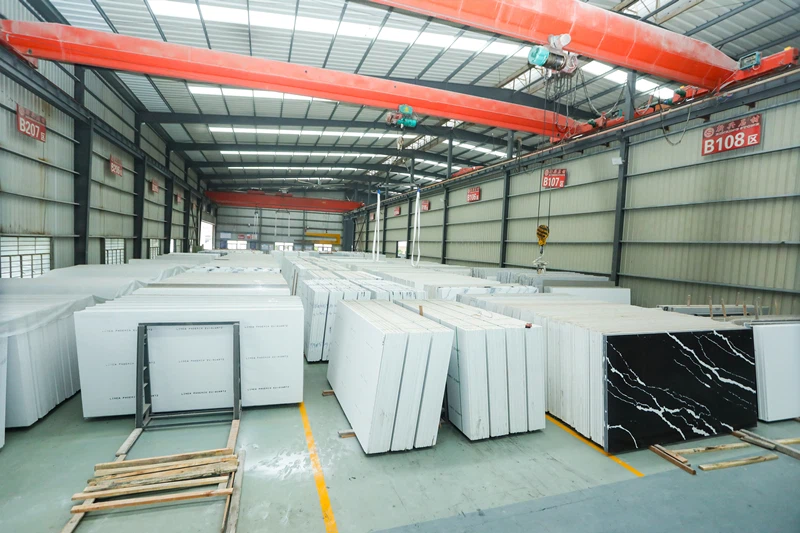
Serving customers across North America, Europe, the Middle East, and Southeast Asia, Nanan Zenlith Co., Ltd. has built a strong reputation for quality, competitive pricing, and dependable delivery—making it a trusted partner for stone solutions worldwide.
Nanan benefits from established industrial clusters, mature quarry networks, and highly concentrated supply chains. This allows manufacturers to access raw materials efficiently while leveraging advanced polishing, sizing, and cutting machinery to maintain competitive pricing and exceptional output volume.
Yes. Top-tier suppliers like Zenlith offer comprehensive OEM and ODM support, accommodating custom color matching, unique slab dimensions, specialized surface textures, and private-label packaging tailored to specific architectural blueprints.
Export orders are packed using fumigation-free wooden crates, reinforced corner protectors, internal shock-absorbing foam, and moisture-barrier film wrapping to withstand cross-ocean freight and inland multi-modal transit without damage.
Products undergo stringent quality checks aligned with global standards such as ISO9001 quality management, CE safety certifications, and ASTM specifications for hardness, slip resistance, water absorption, and chemical durability.
 Zenlith Stone