Explore our top-tier engineered quartz, artificial marble, and sustainable surfaces designed for modern residential and commercial interior architecture.

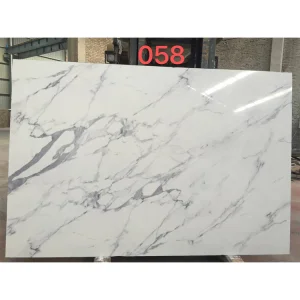
Nanan Zenlith Co., Ltd. is a professional manufacturer and global supplier specializing in artificial marble, quartz stone, and engineered & natural stone solutions for residential, commercial, and architectural applications. Based in Nanan—one of China’s most established stone industry hubs—the company integrates advanced production technology with strict quality control to deliver consistent, high-performance surfaces.
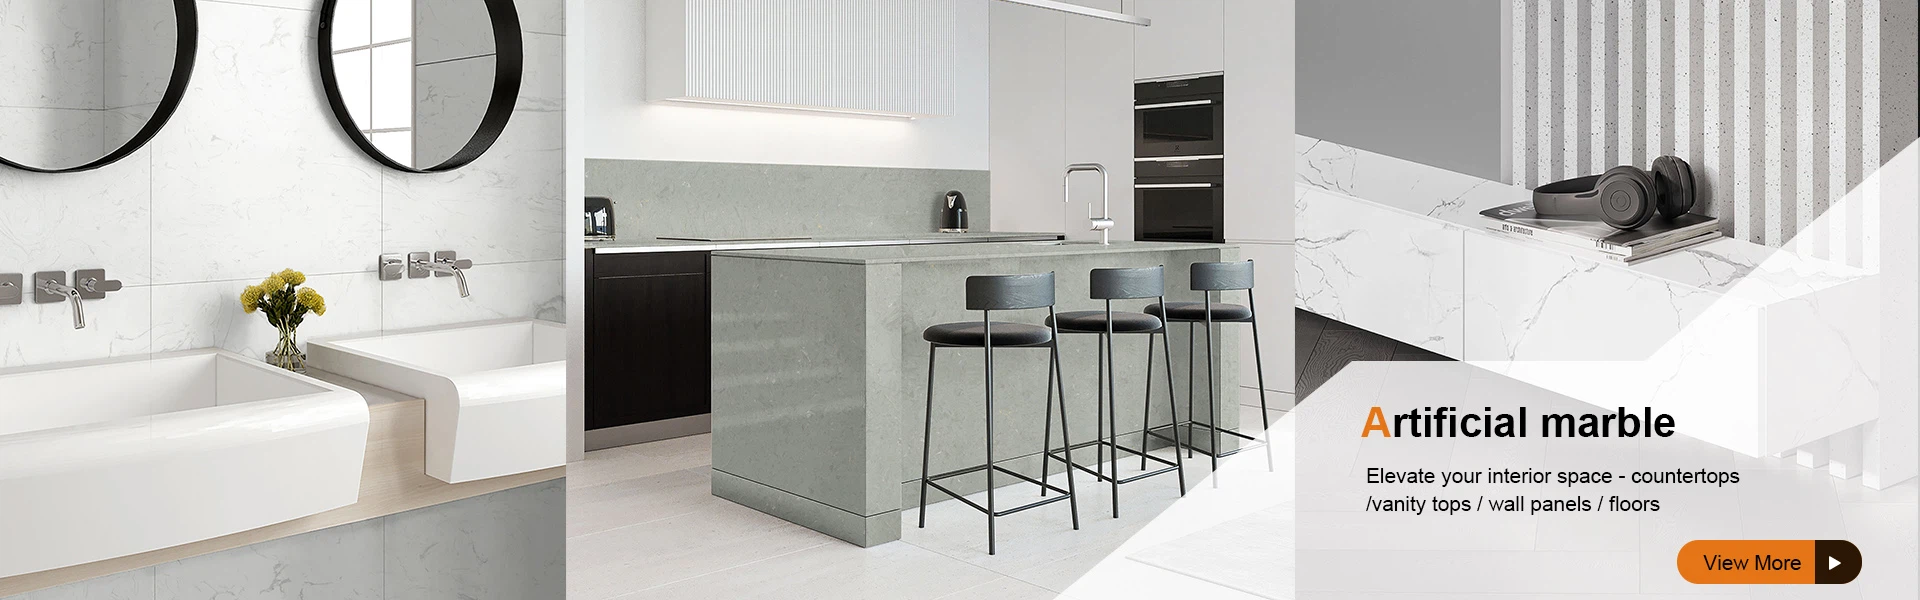
Zenlith’s product portfolio includes artificial marble slabs, engineered quartz surfaces, and a wide selection of natural stones such as granite and marble. Designed to meet modern design and construction demands, its materials are widely used for kitchen countertops, bathroom vanities, wall cladding, flooring systems, and custom interior projects. The company focuses on durability, stain resistance, and aesthetic versatility, offering a variety of colors, textures, and finishes tailored to global market trends.
With a commitment to innovation and sustainability, Zenlith continuously upgrades its manufacturing processes to ensure environmentally responsible production and long-term product reliability. Its experienced team provides OEM/ODM services, supporting clients from material selection and customization to packaging and export logistics.
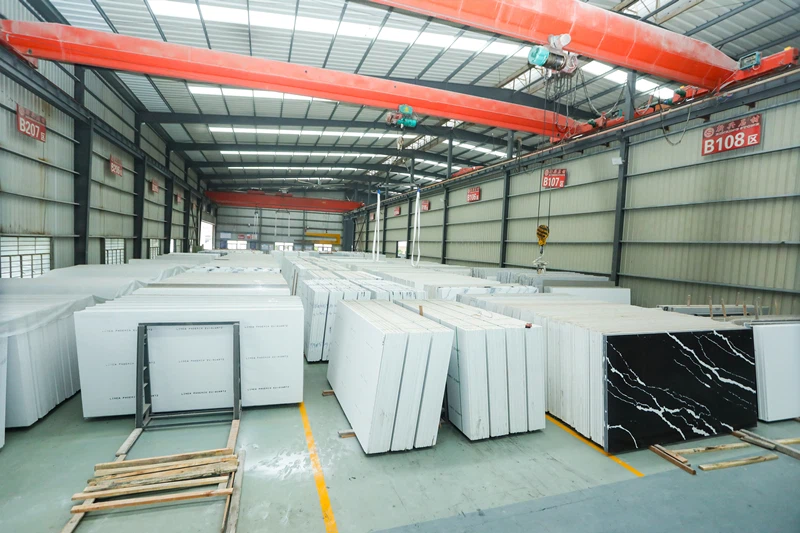
Serving customers across North America, Europe, the Middle East, and Southeast Asia, Nanan Zenlith Co., Ltd. has built a strong reputation for quality, competitive pricing, and dependable delivery—making it a trusted partner for stone solutions worldwide.
Discover our specialized line of sintered slabs, flexible stone veneers, and high-durability composite materials engineered for next-gen architectural demands.


An authoritative analysis on global market trends, manufacturing technology roadmaps, and supply chain resilience in China's leading stone industrial clusters.
From high-traffic commercial retail flooring in North America to luxury hospitality vanity tops in Europe and resilient residential kitchen countertops in the Middle East, our recycled and engineered stone solutions adapt seamlessly to diverse environmental stressors, thermal fluctuations, and structural loads.
Integrating AI-driven color matching, robotic pressing systems, and closed-loop water recycling networks, our manufacturing facilities set new benchmarks in resource efficiency, reducing carbon footprints while maximizing crystalline density and flexural strength.
Anchored in Nanan, the epicenter of global stone processing, Zenlith leverages localized raw material ecosystems, streamlined multi-modal logistics, and robust inventory forecasting to guarantee uninterrupted project fulfillment and highly competitive wholesale pricing.
As international green building codes tighten (LEED, BREEAM), demand for recycled stone aggregates and zero-VOC artificial slabs has surged. Chinese manufacturing leadership provides the scale and precision required by multinational real estate developers.
We provide full regulatory documentation, including NSF, CE, and ISO certifications, ensuring that importers and contractors meet all regional building safety, food contact safety, and environmental compliance standards without friction.
Backed by decades of metallurgical and petrological R&D, our engineering team publishes transparent material testing data, offering architects and specifiers verified technical parameters for load-bearing, abrasion resistance, and chemical inertness.
Expert answers regarding our manufacturing capabilities, customization options, export protocols, and product performance standards.
Zenlith combines decades of stone processing expertise in Nanan with state-of-the-art automated manufacturing lines. We specialize in turning stone byproduct aggregates into high-value, eco-friendly engineered slabs without compromising aesthetic luxury or mechanical durability.
Yes. We offer fully customizable dimensions, thickness profiles (2cm, 3cm, and ultra-thin sintered formats), edge profiling, and surface finishes tailored to specific architectural blueprints and large-scale commercial developments.
Our products undergo rigorous testing for scratch resistance, stain repellence, and flexural strength. They comply with major international standards including ISO9001 quality management, CE marking for European markets, and NSF certification for food contact safety.
We utilize fumigated wooden bundles and crates reinforced with protective corner guards and waterproof interlayers. Our logistics department coordinates closely with global freight carriers to ensure secure, timely delivery to ports worldwide.
 Zenlith Stone